


Grade 5 titanium (Ti-6Al-4V) delivers exceptional strength, corrosion resistance, and thermal stability - but machining a 2mm thin-wall curved cavity cover plate from this material is one of the most challenging problems in precision manufacturing. Here is how it is done.

The Part: Thin, Curved, and Unforgiving
The component in question is a large-radius curved thin-wall cavity cover plate - a sealing enclosure used in aerospace and precision equipment.
| Feature | Specification |
|---|---|
| Wall thickness | 2 mm (uniform throughout the cavity) |
| Shoulder thickness | 6 mm at both connection ends |
| Geometry | Curved, closed-arc cavity structure |
| Sealing surface flatness | ≤ 0.1 mm |
| Surface quality | Smooth, continuous - no chatter marks, dents, edge collapse, or deformation |
A 2mm wall on a curved titanium surface is rigid enough to hold its shape only when machining forces are perfectly controlled. Any vibration, uneven stress, or clamping error shows up immediately as chatter marks, wall thickness deviation, or warping.
The Process: An Integrated Solution
The machining strategy follows a clear principle: shape first, cavity second; rough before fine; stress release between stages; multiple light finishing passes.
Process flow
Raw material preparation → Outer profile roughing and finishing → Mounting hole machining → Convex cavity roughing and finishing → Stress relief treatment → Concave cavity pocketing (rough + finish) → Sealing face precision milling → Precision grinding and lapping → Final inspection
Key process details
Convex cavity machining
- Roughing: High-cobalt four-flute carbide end mill - maximum rigidity and vibration resistance for heavy stock removal. Continuous high-pressure coolant throughout to control temperature and prevent work hardening.
- Finishing: Polycrystalline cubic boron nitride (PCBN) ball-nose mill with surface-following toolpath strategy - uniform cutting load, minimal vibration. Surface error controlled to within 0.012 mm.
Concave cavity machining and deformation control
- Workholding: Custom fixture provides zero-shift, high-rigidity support - eliminates vibration at the source.
- Roughing: Layered pocketing - uniform stock removal prevents local stress concentration.
- Stress relief: Natural aging between roughing and finishing - releases residual cutting stress before final machining.
- Finishing: Multi-pass, repositioned clamp strategy - corrects reference alignment, eliminates cumulative clamping error, ensures uniform 2mm wall thickness throughout.
Sealing face precision forming
Precision milling removes stock and toolpath marks
Precision grinding followed by lapping - progressive micro-shaping
In-process measurement throughout - real-time correction of flatness deviation
Final flatness: ≤ 0.1 mm, consistently achieved

What Makes This Work
| Factor | Solution |
|---|---|
| Chatter | High-rigidity tooling + PCBN finishing + high-pressure coolant |
| Thin-wall deformation | Custom fixture + layered stock removal + natural aging between stages |
| Springback after unclamping | Multi-pass repositioned finishing - eliminates cumulative clamp error |
| Flatness control | Precision milling → grinding → lapping with in-process measurement |
| Residual stress | Stress relief treatment inserted between roughing and finishing |
The proven formula: rigid workholding, layered stock removal, stress relief, and multiple light finishing passes - applied with disciplined process control.
This level of machining precision is only achievable when the starting titanium plate has verified material quality. A 2mm thin-wall cavity cover demands:
| Material Requirement | Why It Matters |
|---|---|
| Uniform wall thickness in the raw plate | Any thickness variation propagates into the finished cavity wall |
| Consistent chemistry and microstructure | Predictable cutting behavior - no localized hardness variations |
| Flat, stress-relieved starting material | Minimizes machining distortion from the first pass |
| Surface cleanliness | No inclusions, laps, or surface defects that could initiate cracking at 2mm wall |
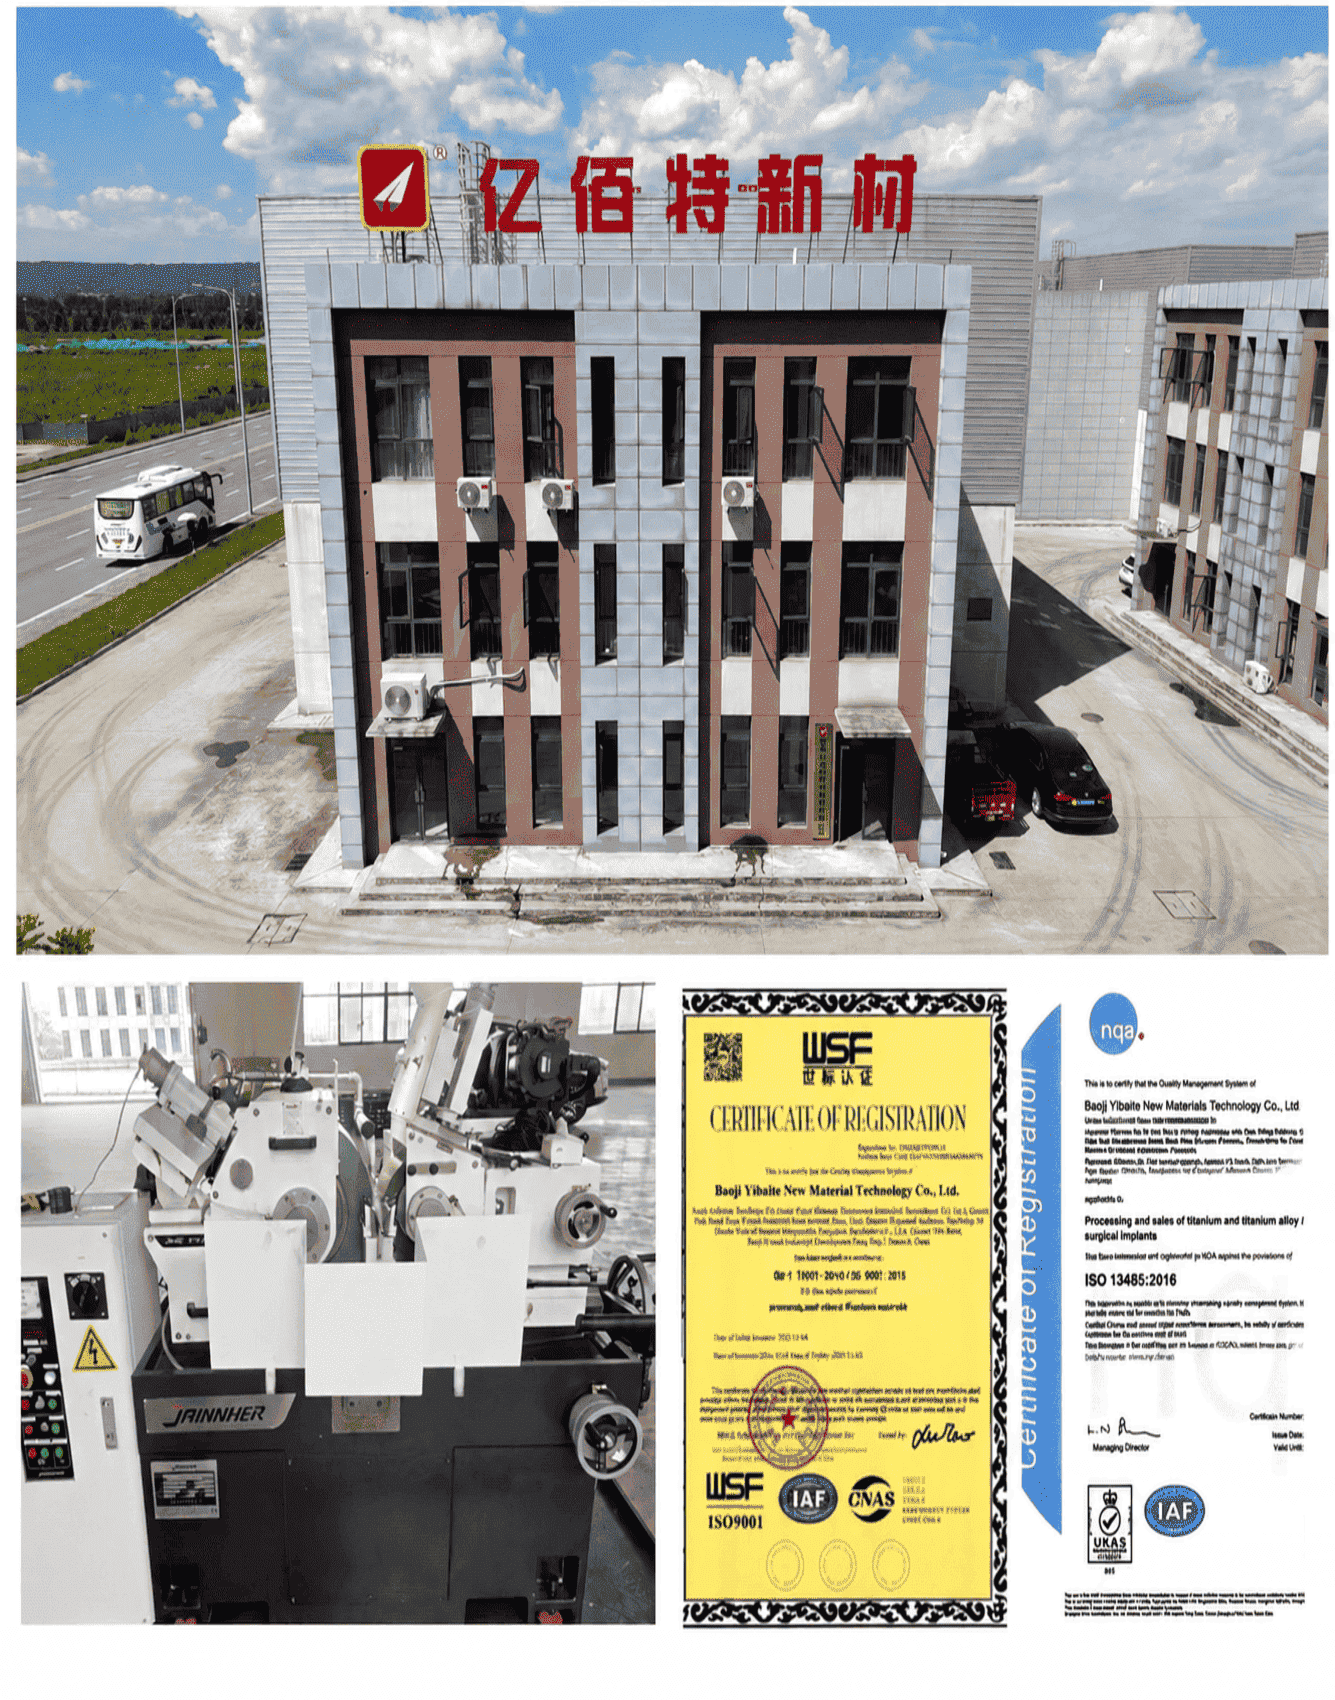
Baoji Yibaite New Materials Technology Co., Ltd. is a high-tech titanium processing company in Baoji, Shaanxi Province - China's Titanium Valley. All products ship with full mill test certificates - chemistry, mechanical properties, dimensions - traceable from ingot to delivered product.
Whether you are a precision machining shop producing thin-wall titanium components, an aerospace manufacturer sourcing plate for enclosure fabrication, or a distributor serving the high-precision titanium market - we are ready to discuss your material requirements.
The Takeaway
Machining a 2mm thin-wall curved cavity cover from Grade 5 titanium is not a single technique - it is an integrated system of tooling, fixturing, process sequencing, stress management, and in-process measurement. But even the best machining process cannot compensate for inconsistent raw material. The precision starts with the plate.
From quality titanium plate in China's Titanium Valley to a 0.012 mm cavity surface in your finished assembly.
FAQ
Q: Why is Grade 5 titanium so difficult to machine at 2mm wall thickness?
A: Low thermal conductivity causes heat buildup and chatter. Low elastic modulus causes springback. At 2mm wall thickness, the workpiece has minimal rigidity - amplifying both problems. Specialized tooling, rigid fixturing, and stress relief between machining stages are essential.
Q: What tolerance can be achieved on thin-wall titanium cavity surfaces?
A: With optimized tooling and process parameters, surface errors can be controlled within 0.012 mm on curved cavity surfaces. Sealing face flatness of ≤ 0.1 mm is achievable through precision milling, grinding, and lapping with in-process measurement.
Q: What raw material form is needed for machining thin-wall cavity covers?
A: Precision-machined thin-wall cavity covers are typically produced from Grade 5 titanium plate - cold-rolled, annealed, and supplied with tight thickness tolerance and verified flatness. Material consistency directly determines machining outcomes
Baoji Yibaite New Materials Technology Co., Ltd. China's Titanium Valley - Your Trusted Titanium Partner.
📧 stevenwei@yibaite.com.cn
📱 WhatsApp: +86 18992799610
🌐 www.ybtti.com